


WEST SYSTEM® | Epoxy Basics | Guide 05
Epoxy bonding surfaces must be clean, dry and sanded. Nearly every adhesion failure we are asked to diagnose comes back to one of those three.
The strength of an epoxy joint depends not only on the epoxy but on how well it adheres to the substrate. Unless you are bonding to partially cured epoxy, the bond relies on the epoxy mechanically keying into the surface — so the three steps below are critical to both primary and secondary bonding, and to fairing and laminating as well.
Preparation guidance from WEST SYSTEM instructional material. Refer to the current technical data sheet for full product specifications and suitability.
3 steps
For good adhesion, epoxy bonding surfaces should be clean, dry and sanded — carried out in that order.
Epoxy bonding surfaces must be free of any contaminants such as grease, oil, wax or mould release. Clean contaminated surfaces with lacquer thinner, acetone or another appropriate solvent. Wipe the surface with paper towels before the solvent dries.
Clean surfaces before sanding, so the contaminant is not sanded into the surface. Follow all safety precautions when working with solvents.
All epoxy bonding surfaces must be as dry as possible for good adhesion. Accelerate drying by warming the bonding surface with a hot air gun, hairdryer or heat lamp, and use fans to move air in confined or enclosed spaces.
Watch for condensation when working outdoors, or whenever the temperature of the work environment changes.
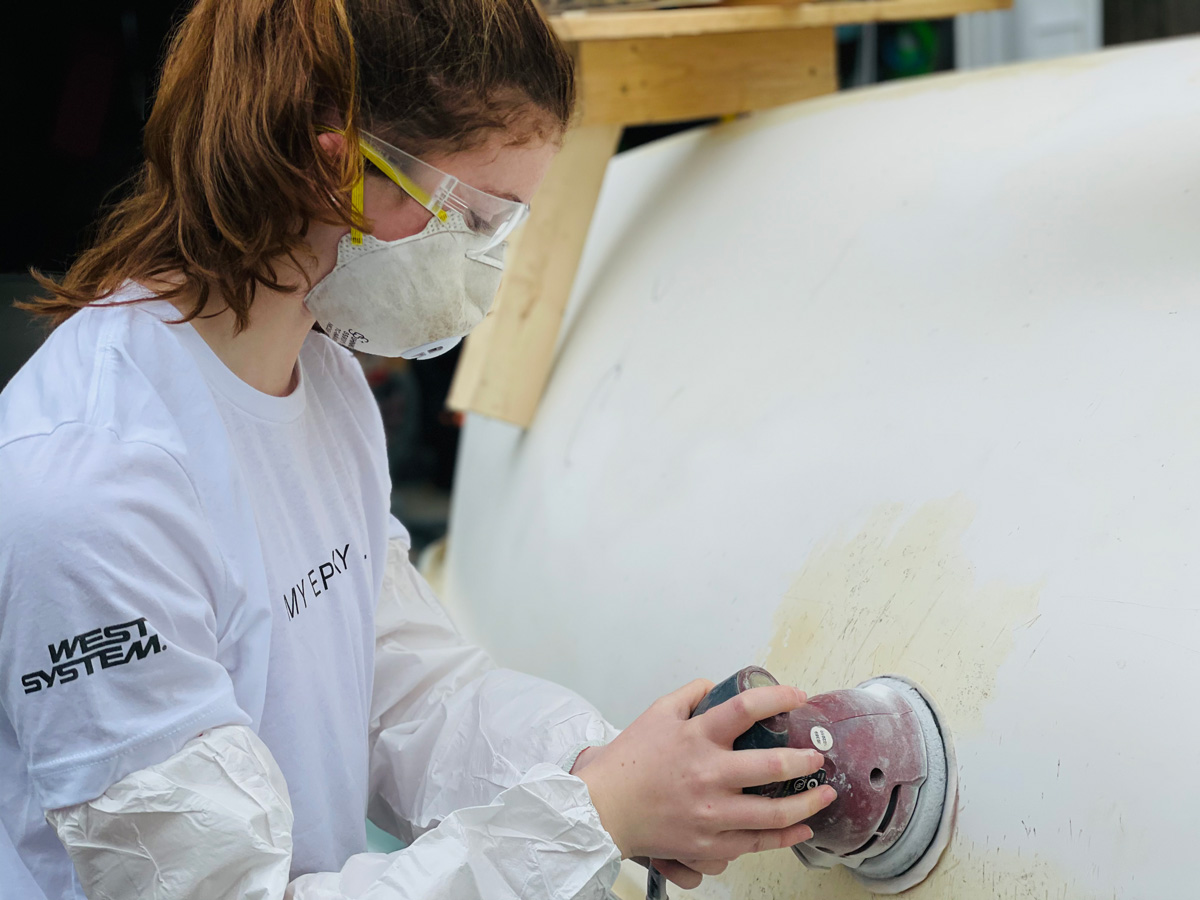
Before applying epoxy, thoroughly abrade smooth non-porous surfaces. 80-grit aluminium oxide paper provides a good texture for the epoxy to key into.
Be sure the surface to be bonded is solid: remove any flaking, chalking, blistering or old coating before sanding, and remove all dust afterwards.
Quick reference
| Material | Preparation | Abrasive |
|---|---|---|
| Hardwoods | Sand before applying epoxy. | 80 grit |
| Porous timbers | No special preparation. If the surface has been burnished by a dull planer or saw blade, sand to open the pores and remove dust. | 80 grit if burnished |
| Teak and oily timbers | Wipe with acetone 15 minutes before coating — solvent removes the oil at the surface and lets the epoxy penetrate. Be sure the solvent has evaporated before coating. G/flex® Epoxy is optimum for oily species. | Acetone wipe |
| Steel or lead | Remove contamination, then sand or grind to bright metal. Coat with epoxy, sand fresh epoxy into the surface, then re-coat or bond after the first coat gels. | Sand or grind to bright metal |
| Aluminium | Dry sand before applying the epoxy. | 80 grit dry |
| Polyester laminates | Clean contamination with a silicone and wax remover such as DuPont Prep-Sol™ 3919S, then sand to a dull finish before applying epoxy. | 80 grit |
| Plastics | Adhesion varies. G/flex® epoxy is the optimum choice. Hard rigid plastics such as PVC, ABS and styrene achieve better adhesion with good preparation and adequate bonding area; after sanding, flame oxidising (passing a propane torch quickly over the surface without melting it) can improve adhesion on some plastics. Always test an unfamiliar plastic. | Sand then test |
| Cured epoxy | Wash off amine blush with clean water and an abrasive pad, dry with paper towels, then sand any remaining gloss. Partially cured epoxy may be bonded to or coated without washing or sanding. | 80 grit after washing |
Guide only. Refer to the current technical data sheet for full product specifications and suitability, and run an adhesion test on any substrate you are unsure of.
Recoating
Unless you are using the blush-free 207 Special Clear Hardener®, amine blush may appear as a wax-like film on cured epoxy surfaces. It is a by-product of the curing process and is more noticeable in cool, moist conditions. Blush can clog sandpaper and inhibit subsequent bonding, but this inert substance is easily removed.
To remove it, wash the surface with clean water — not solvent — and an abrasive pad such as a Scotch-Brite™ 7447 general purpose hand pad. Dry the surface with paper towels to lift the dissolved blush before it dries back onto the surface, then sand any remaining glossy areas with 80-grit paper. Wet-sanding also removes amine blush. If a release fabric was applied over the fresh epoxy, the blush comes away with the fabric and no additional sanding is required.
Epoxy surfaces that have not fully cured may be bonded to or coated with epoxy without washing or sanding. Before applying coatings other than epoxy — paints, antifouling, varnishes, gelcoats — allow the epoxy to cure fully, then wash and sand. See Finish Coatings.
3 sources
There is no good reason to wipe a surface with an organic solvent unless there is evidence that an organic contaminant is present. Solvents such as acetone, lacquer thinner and proprietary mixtures like DuPont Prep-Sol™ will remove oil, grease and wax.
But wiping with solvent can also dissolve contaminants out of the rag and deposit them on the work surface, where they prevent adhesion. Silicone is a well-known mould release and an ingredient in many fabric softeners, so it is readily transferred from a laundered rag. Many organic solvents also dissolve the man-made fibres in rags — an acetone wipe-down can leave plastic on the surface you are trying to clean, acting exactly like a mould release.
If you do suspect a contaminant that needs solvent, use plain white paper towels to apply it and fresh paper towels to dry the surface. Do not use rags. Wipe the solvent off while it is still wet so the contaminant is not re-deposited, and change paper towels frequently.
Despite the dust, a freshly sanded surface is about as clean as a surface gets. Do not rub a bare hand over it to check for smoothness: skin deposits oils, and the salt on your skin can accelerate corrosion on metal and cause adhesion problems. Wear a clean glove.
Vacuum the dust off, sweep it off with an uncontaminated bench brush, or wash it off with water. You do not need to remove every last particle — remaining sanding dust has no more effect on adhesion than an epoxy filler.
Sticky tack rags are a different matter. Most paints and varnishes contain enough solvent to dissolve the residue a tack rag leaves; epoxy contains none of those aggressive solvents, so that residue can cause adhesion problems and fisheyes in subsequent coats. Use a dry tack cloth that leaves no residue. Do not use compressed air, which may carry compressor oil or water onto the surface.
Some workshop heat sources contaminate surfaces. Torpedo or salamander heaters do not burn cleanly and can exhaust large amounts of moisture and hydrocarbons that accumulate quickly on a work surface.
Zinc stearate is applied to some sandpapers to stop them loading. Stearate is chemically similar to animal fat and can contaminate a surface through sanding alone — use aluminium oxide or untreated waterproof wet-and-dry paper instead.
Amine blush is water-soluble but resists most organic solvents. Wash epoxy surfaces with water clean enough to drink, using a Scotch-Brite™ pad or wet-and-dry paper, and dry with paper towels. Soapy water, or water with ammonia or bleach, is unnecessary and can leave its own residue.
Water break test
Wash it with water. The unsophisticated water break test works because many contaminants repel water. Apply water to the surface with a Scotch-Brite™ pad: if the water sheets off evenly, the part is clean; if it channels or beads in certain areas, the surface needs more cleaning.
The test works equally well on small and large parts. The water used must be free of surfactants or other contamination that would let it flow evenly even where the surface is dirty. It will not reveal soap residues or other water-soluble films, though it will help remove them.
There are materials epoxy does not adhere to well no matter how the surface is cleaned. But most adhesion problems trace back to some form of surface contamination — subtle or obvious — and when you absolutely must have good adhesion, the substrate must be clean.
Discuss your process requirements with our technical team. If you are bonding an unfamiliar substrate, or diagnosing an adhesion failure, contact ATL Composites before committing to a full lay-up.
4 questions
80-grit aluminium oxide paper. It leaves the texture epoxy needs to key into a smooth, non-porous surface. Avoid stearate-treated papers, which can contaminate the surface as you sand.
Only if there is evidence of an organic contaminant such as oil, grease or wax. An unnecessary solvent wipe can make things worse by depositing silicone or dissolved rag fibres onto the surface. If you do use solvent, apply and remove it with clean white paper towels — never rags — and wipe it off while still wet.
Wash with clean water and an abrasive pad, then dry with paper towels before the dissolved blush dries back on. Sand remaining gloss with 80-grit paper, or wet-sand. Solvents do not remove blush. 207 Special Clear Hardener® is blush-free.
A simple check for surface cleanliness: wet the surface with clean water using a Scotch-Brite™ pad. If the water sheets off evenly the surface is clean; if it beads or channels, contamination is still present and the surface needs further cleaning.
Supplied by ATL Composites
Resin & hardeners
105 Epoxy Resin with 205 Fast, 206 Slow, 207 Special Clear and 209 Extra Slow Hardeners.
Toughened adhesive
Toughened epoxy adhesive for oily timbers, plastics and substrates that move.
Browse the full WEST SYSTEM range supplied by ATL Composites.
View the WEST SYSTEM rangeGuide only. Adapted from WEST SYSTEM instructional material (original guide). Read the product label and the current technical and safety data sheets before use.
Guide 05 of 11
Discuss your process requirements with our technical team on +61 7 5563 1222 or [email protected].
WEST SYSTEM®, 105 Epoxy Resin®, 207 Special Clear Hardener® and G/flex® are registered trademarks of Gougeon Brothers, Inc., USA. Manufactured and distributed in Australia by ATL Composites Pty Ltd. Scotch-Brite™ is a trademark of 3M; Prep-Sol™ of DuPont. Diagrams and instructions courtesy of WEST SYSTEM.